
Tap Drill Size Chart: UNC, UNF, Metric & NPT (Printable)
A tap drill is the drill you use to make a hole before cutting threads into it with a tap. Pick a drill that is too small and the tap binds or snaps; too large and the thread strips. This tap drill size chart lists the correct drill for every common UNC, UNF, metric and NPT thread, along with clearance hole sizes, so you can find the right bit in seconds.
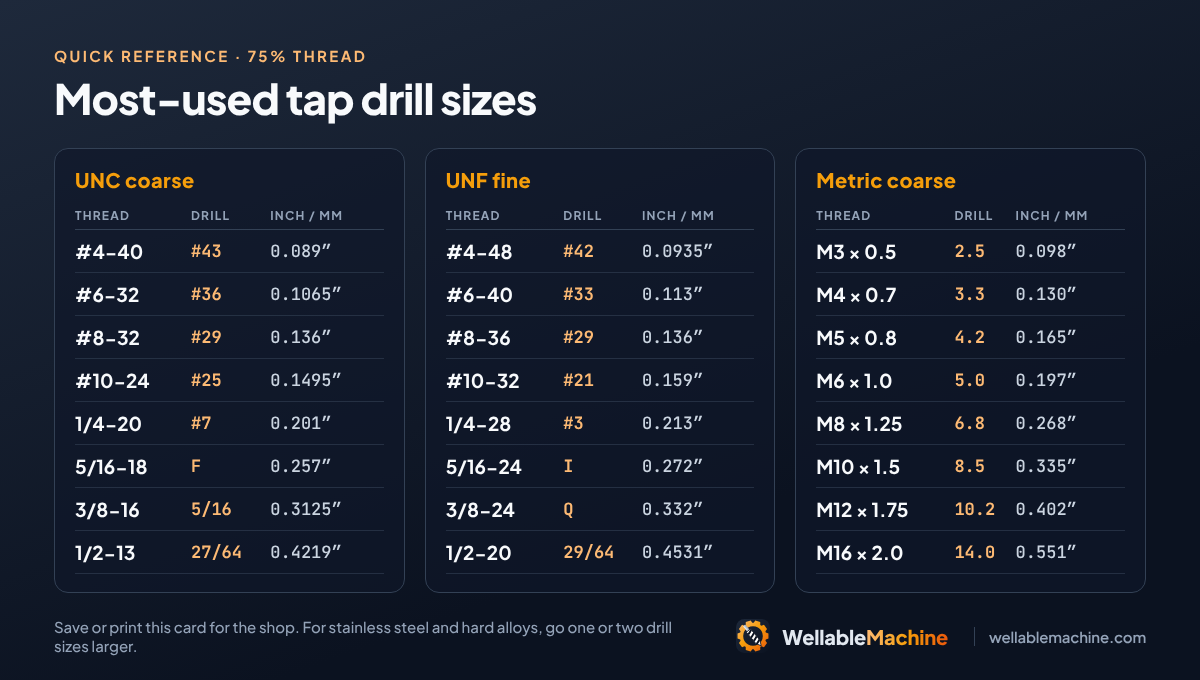
All inch tap drills below give roughly a 75% thread, the industry standard for steel, aluminum, brass and cast iron. Metric tap drills use the simple rule major diameter − pitch. If you’re tapping stainless steel or another tough material by hand, go one or two sizes larger; we explain why further down.
How to Read a Thread Size
Every thread callout tells you two things: the diameter and how fine the thread is. Inch threads list diameter and threads per inch (TPI); metric threads list diameter and pitch in millimeters.
- 1/4-20 UNC: 1/4 in diameter, 20 threads per inch, Unified Coarse series.
- 10-32 UNF: #10 screw gauge (0.190 in), 32 threads per inch, Unified Fine series.
- M8 × 1.25: 8 mm diameter, 1.25 mm between threads. If no pitch is given (just “M8”), it means the coarse pitch.
- 1/8-27 NPT: a tapered pipe thread for a nominal 1/8 in pipe, 27 threads per inch.
The Unified Thread Standard (ASME B1.1) defines the inch sizes, and ISO metric screw threads cover the metric ones.
UNC Tap Drill Size Chart (Coarse Thread)
Coarse threads are the most common for general hardware and are more forgiving in soft materials.
| Thread | Tap drill (75%) | Decimal (in) | Close-fit clearance | Free-fit clearance |
|---|---|---|---|---|
| #2-56 | #50 | 0.0700 | #43 (0.089) | #41 (0.096) |
| #4-40 | #43 | 0.0890 | #32 (0.116) | #30 (0.1285) |
| #6-32 | #36 | 0.1065 | #27 (0.144) | #25 (0.1495) |
| #8-32 | #29 | 0.1360 | #18 (0.1695) | #16 (0.177) |
| #10-24 | #25 | 0.1495 | #9 (0.196) | #7 (0.201) |
| #12-24 | #16 | 0.1770 | #2 (0.221) | #1 (0.228) |
| 1/4-20 | #7 | 0.2010 | F (0.257) | H (0.266) |
| 5/16-18 | F | 0.2570 | P (0.323) | Q (0.332) |
| 3/8-16 | 5/16 | 0.3125 | W (0.386) | X (0.397) |
| 7/16-14 | U | 0.3680 | 29/64 (0.4531) | 15/32 (0.4688) |
| 1/2-13 | 27/64 | 0.4219 | 33/64 (0.5156) | 17/32 (0.5312) |
| 9/16-12 | 31/64 | 0.4844 | 37/64 (0.5781) | 19/32 (0.5938) |
| 5/8-11 | 17/32 | 0.5312 | 41/64 (0.6406) | 21/32 (0.6562) |
| 3/4-10 | 21/32 | 0.6562 | 49/64 (0.7656) | 25/32 (0.7812) |
| 7/8-9 | 49/64 | 0.7656 | 57/64 (0.8906) | 29/32 (0.9062) |
| 1-8 | 7/8 | 0.8750 | 1-1/64 (1.0156) | 1-1/32 (1.0312) |
UNF Tap Drill Size Chart (Fine Thread)
Fine threads have shallower teeth, so they need a slightly larger tap drill than the coarse thread of the same diameter. They’re used in thin walls, for fine adjustment and where vibration is a concern. Clearance holes are the same as the UNC table above.
| Thread | Tap drill (75%) | Decimal (in) | Metric near-equivalent |
|---|---|---|---|
| #4-48 | #42 | 0.0935 | 2.4 mm |
| #6-40 | #33 | 0.1130 | 2.9 mm |
| #8-36 | #29 | 0.1360 | 3.5 mm |
| #10-32 | #21 | 0.1590 | 4.0 mm |
| #12-28 | #14 | 0.1820 | 4.6 mm |
| 1/4-28 | #3 | 0.2130 | 5.4 mm |
| 5/16-24 | I | 0.2720 | 6.9 mm |
| 3/8-24 | Q | 0.3320 | 8.4 mm |
| 7/16-20 | 25/64 | 0.3906 | 9.9 mm |
| 1/2-20 | 29/64 | 0.4531 | 11.5 mm |
| 9/16-18 | 33/64 | 0.5156 | 13.1 mm |
| 5/8-18 | 37/64 | 0.5781 | 14.7 mm |
| 3/4-16 | 11/16 | 0.6875 | 17.5 mm |
| 7/8-14 | 13/16 | 0.8125 | 20.6 mm |
| 1-12 | 15/16 | 0.9375 | 23.8 mm |
Metric Tap Drill Size Chart (Coarse and Fine)
For metric threads, the tap drill is simply the major diameter minus the pitch. An M6 × 1.0 thread uses a 6 − 1 = 5.0 mm drill. Clearance sizes follow ISO 273.
| Thread | Pitch (mm) | Tap drill (mm) | Inch equivalent | Close clearance | Normal clearance |
|---|---|---|---|---|---|
| M2 | 0.4 | 1.6 | #52 / 1/16 | 2.2 | 2.4 |
| M2.5 | 0.45 | 2.05 | #46 | 2.7 | 2.9 |
| M3 | 0.5 | 2.5 | #39 | 3.2 | 3.4 |
| M4 | 0.7 | 3.3 | #30 | 4.3 | 4.5 |
| M5 | 0.8 | 4.2 | #19 | 5.3 | 5.5 |
| M6 | 1.0 | 5.0 | #9 | 6.4 | 6.6 |
| M8 | 1.25 | 6.8 | H | 8.4 | 9.0 |
| M8 fine | 1.0 | 7.0 | J | 8.4 | 9.0 |
| M10 | 1.5 | 8.5 | Q | 10.5 | 11.0 |
| M10 fine | 1.25 | 8.8 | 11/32 | 10.5 | 11.0 |
| M12 | 1.75 | 10.2 | Y | 13.0 | 13.5 |
| M12 fine | 1.5 | 10.5 | Z | 13.0 | 13.5 |
| M14 | 2.0 | 12.0 | 15/32 | 15.0 | 15.5 |
| M16 | 2.0 | 14.0 | 35/64 | 17.0 | 17.5 |
| M20 | 2.5 | 17.5 | 11/16 | 21.0 | 22.0 |
| M24 | 3.0 | 21.0 | 53/64 | 25.0 | 26.0 |
NPT Pipe Thread Tap Drill Chart
NPT threads are tapered (1/16 in per inch), so the tap cuts deeper as it goes in. The drill sizes below are for tapping without a taper reamer, which is how most shops do it. Tap only until a fitting threads in hand-tight about 3–4 turns.
| Pipe size | TPI | Tap drill | Decimal (in) |
|---|---|---|---|
| 1/16 NPT | 27 | D | 0.246 |
| 1/8 NPT | 27 | R | 0.339 |
| 1/4 NPT | 18 | 7/16 | 0.4375 |
| 3/8 NPT | 18 | 37/64 | 0.5781 |
| 1/2 NPT | 14 | 23/32 | 0.7188 |
| 3/4 NPT | 14 | 59/64 | 0.9219 |
| 1 NPT | 11.5 | 1-5/32 | 1.1563 |
| 1-1/4 NPT | 11.5 | 1-1/2 | 1.5000 |
| 1-1/2 NPT | 11.5 | 1-47/64 | 1.7344 |
| 2 NPT | 11.5 | 2-7/32 | 2.2188 |
How to Calculate a Tap Drill Size
You don’t need a chart if you remember two formulas.
- Inch threads (75%): tap drill ≈ major diameter − (0.974 ÷ TPI). For 1/4-20: 0.250 − 0.0487 = 0.201 in, which is a #7 drill.
- Metric threads: tap drill = major diameter − pitch. For M8 × 1.25: 8 − 1.25 = 6.75 mm, so use 6.8 mm.
- Thread percentage for any drill: % thread = 76.98 × TPI × (major diameter − drill diameter).

Choosing a Larger Drill for Hard Materials
A 75% thread is only slightly stronger than a 60–65% thread, but it takes much more force to tap. That extra force is what snaps taps in stainless steel, titanium and hardened alloys. Many machinists drill one or two sizes larger in these materials. For example, use a #5 or 5.2 mm drill instead of #7 for 1/4-20 in stainless. For drilling tips in tough metals, read our guide on how to drill stainless steel and see our picks for the best drill bits for stainless steel.
Cutting Taps vs. Forming Taps
Everything in the tables above is for standard cutting taps, which remove metal to form the thread. Forming (roll) taps push the metal into shape without making chips and need a noticeably larger hole, roughly halfway between the tap drill and the major diameter. For example, a 1/4-20 forming tap uses about a 0.228 in hole instead of 0.201 in. Forming taps work best in aluminum, copper, brass and mild steel. Always use the forming-tap chart from the tap’s manufacturer.
Tips for Clean, Strong Threads
- Drill straight. A crooked hole makes a crooked thread. Use a drill press or a drill guide when you can.
- Chamfer the hole with a countersink so the tap starts square and the first thread isn’t raised.
- Use cutting fluid for both drilling and tapping. Sulfur-based oil works well in steel; a light oil or tapping fluid is fine in aluminum.
- Break the chip with hand taps: turn forward half a turn, back a quarter turn.
- Choose the right tap: spiral-point (gun) taps for through-holes, spiral-flute taps for blind holes, and a bottoming tap to finish threads at the bottom of a blind hole.
- Drill blind holes deeper than the thread you need, by at least 3–4 pitches.
Frequently Asked Questions
What is a tap drill?
It’s the drill bit used to make the hole before tapping. Its diameter is a little larger than the thread’s minor diameter so the tap has metal to cut into without binding.
What size drill for a 1/4-20 tap?
A #7 drill (0.201 in) or 13/64 in. See our full 1/4-20 tap drill size guide.
What size drill for a 10-32 tap?
A #21 drill (0.159 in). See the 10-32 tap drill size guide for metric and stainless options.
What size drill for a 3/8-16 tap?
A 5/16 in drill (0.3125 in). Details are in our 3/8-16 tap drill size guide.
What size drill for an M6 tap?
5.0 mm for a standard M6 × 1.0 thread. If you only have inch bits, a #9 (0.196 in) is the closest.
What size drill for a 1/8 NPT tap?
A letter R drill (0.339 in). An 11/32 in drill is a common substitute.
Why is the tap drill smaller than the bolt?
The tap needs material to cut the thread’s teeth. The hole is sized close to the thread’s minor (root) diameter, and the tap cuts outward to the full major diameter.
What is the difference between a tap drill and a clearance drill?
A tap drill makes a hole to be threaded. A clearance drill makes a hole slightly larger than the bolt so it can pass through freely without threads.
Where can I see all the number and letter drill sizes?
This drill bit sizes reference lists the full number, letter and fractional series with decimal equivalents.