1/2-13 Tap Drill Size: 27/64 Drill Chart, Clearance & Metric
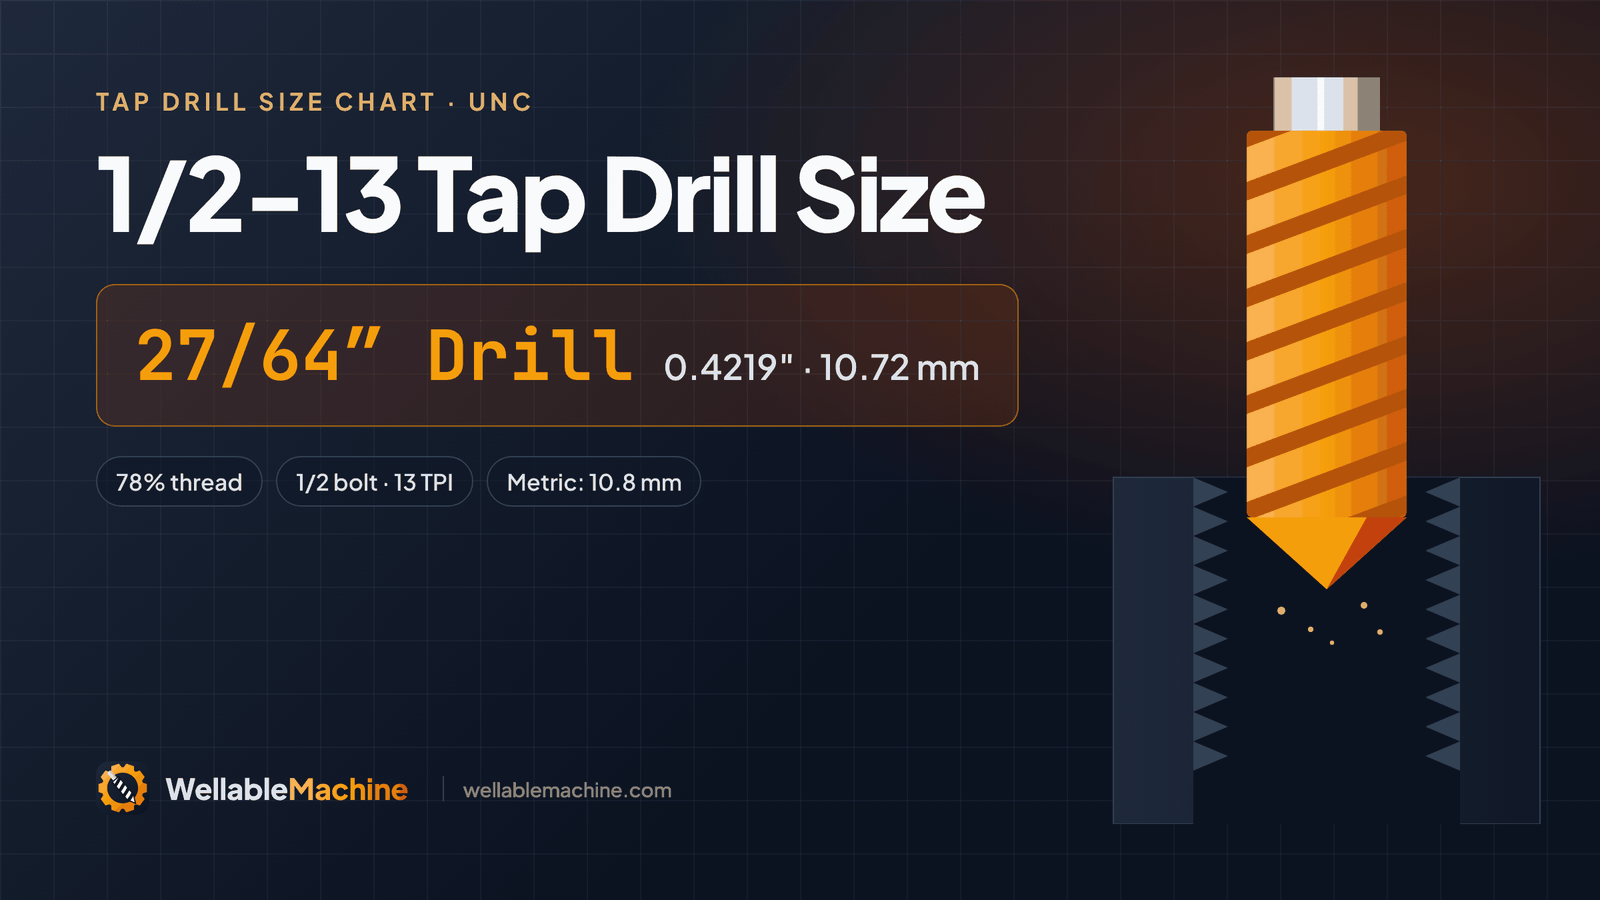
Quick answer: the standard tap drill for a 1/2-13 UNC thread is a 27/64 in drill (0.4219 in / 10.72 mm). It gives about a 78% thread, the normal choice for steel, cast iron, aluminum and brass. With metric drills, use 10.8 mm (about 75%). When hand tapping steel or stainless, a 7/16 in drill (0.4375 in) cuts tapping torque a lot and still gives a strong thread.
A 1/2-13 tap is a big tool that takes real effort to turn, so getting the hole right saves both time and taps. This guide covers the full 1/2-13 drill chart, clearance holes, the 1/2-20 fine-thread drill, forming-tap and Heli-Coil sizes, and how to drill a half-inch tap hole cleanly with a hand drill or a drill press.
1/2-13 Thread Specifications at a Glance
“1/2-13” means a 1/2 in nominal diameter bolt with 13 threads per inch. It is the coarse (UNC) thread for this size in the Unified Thread Standard, used on structural brackets, machinery mounts, vises, trailer hitches and heavy fixtures.
| Specification | Value |
|---|---|
| Thread series | UNC (Unified National Coarse) |
| Major diameter | 0.500 in (12.70 mm) |
| Threads per inch | 13 |
| Pitch | 0.0769 in (1.954 mm) |
| Basic minor diameter | 0.4056 in (10.30 mm) |
| Tap drill, ~75% thread | 27/64 = 0.4219 in (10.72 mm) |
| Tap drill, 50% thread | 29/64 = 0.4531 in (11.51 mm) |
| Close-fit clearance | 33/64 = 0.5156 in (13.10 mm) |
| Free-fit clearance | 17/32 = 0.5312 in (13.49 mm) |
| Hex head wrench size | 3/4 in |
1/2-13 Tap Drill Size Chart by Thread Percentage
With large taps, the torque difference between a 78% and a 65% thread is huge, while the strength difference is small. That’s why experienced machinists often drill a little larger for hand tapping. The percentages below use % thread = 76.98 × TPI × (major diameter − drill diameter).
| Drill | Inches | mm | Approx. thread | When to use it |
|---|---|---|---|---|
| 10.5 mm | 0.4134 | 10.50 | 87% | Too tight; hard to tap |
| 10.7 mm | 0.4213 | 10.70 | 79% | Metric twin of 27/64 |
| 27/64 | 0.4219 | 10.72 | 78% | Standard for most materials |
| 10.8 mm | 0.4252 | 10.80 | 75% | Most common metric option |
| 11.0 mm | 0.4331 | 11.00 | 67% | Steel, easier hand tapping |
| 7/16 | 0.4375 | 11.11 | 63% | Stainless, hand tapping large holes |
| 29/64 | 0.4531 | 11.51 | 47% | Very hard alloys; minimum thread |
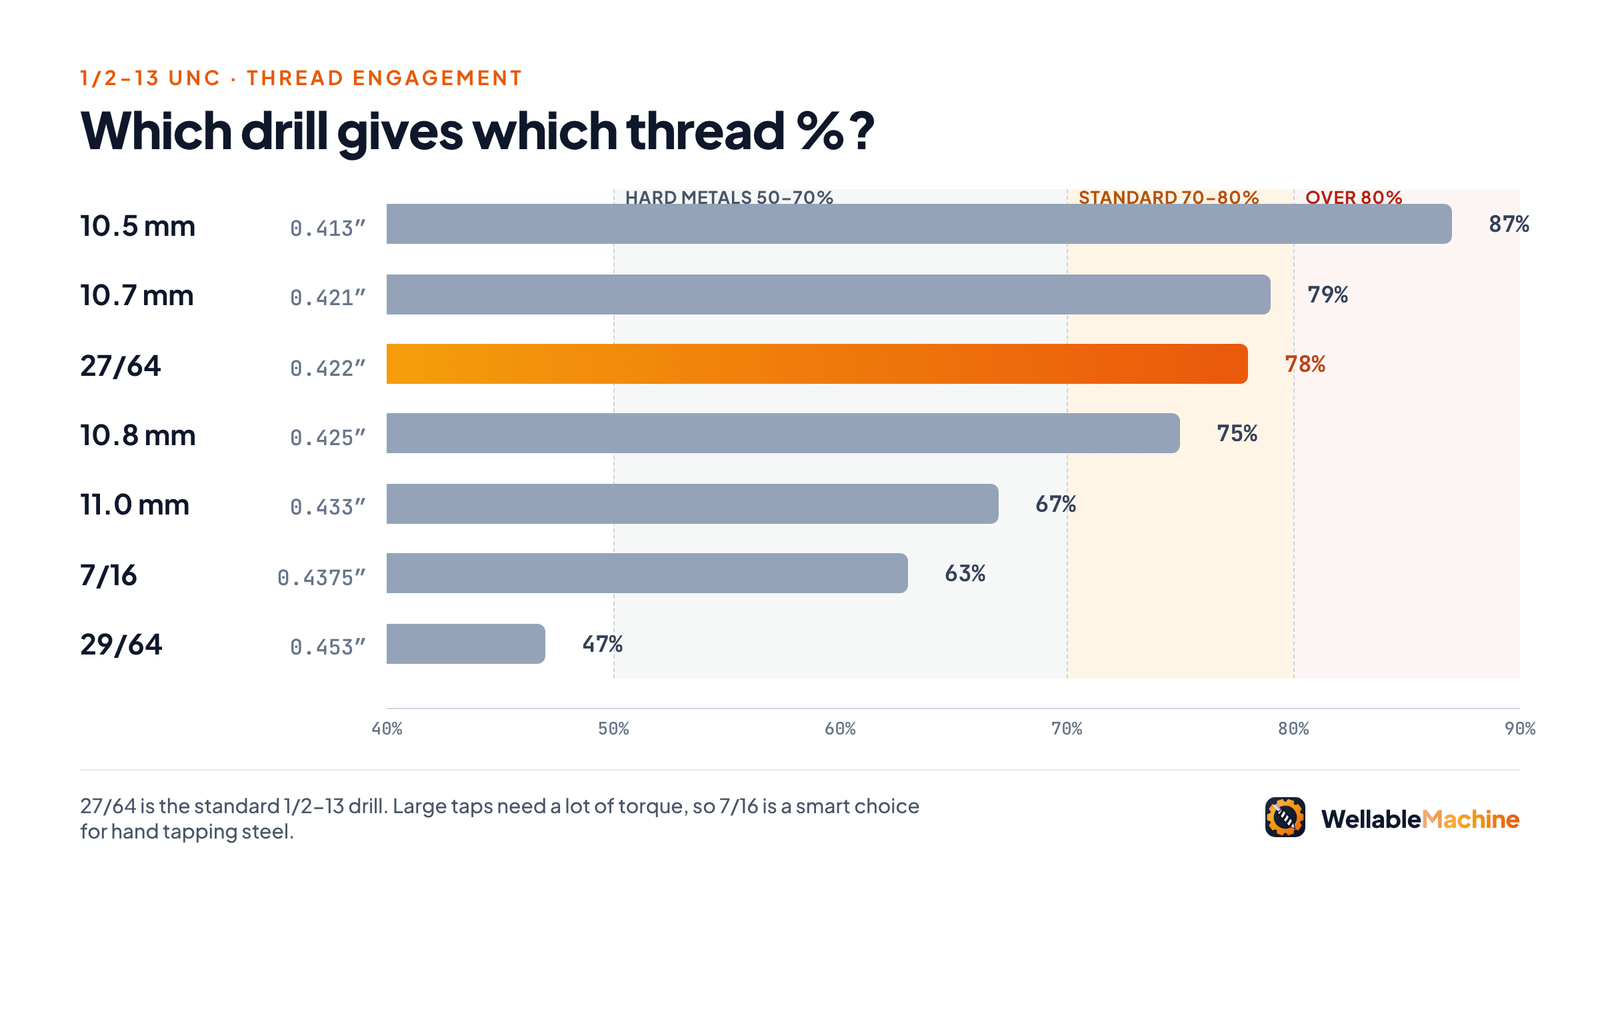
Which drill should you use? Use 27/64 in for machine tapping and for aluminum, brass and cast iron. For hand tapping steel, a 7/16 in drill is a smart choice: it’s in nearly every fractional set, it makes the tap much easier to turn, and a 63% thread on a 1/2 in bolt is still stronger than the bolt in most joints. In stainless, 7/16 in is the practical standard.
Clearance Hole Sizes for a 1/2 in Bolt
| Fit | Drill | Inches | mm | Use it for |
|---|---|---|---|---|
| Close fit | 33/64 | 0.5156 | 13.10 | Accurate location of mating parts |
| Free fit | 17/32 | 0.5312 | 13.49 | General assemblies |
| Loose fit | 9/16 | 0.5625 | 14.29 | Structural steel, hole patterns, welded frames |
1/2-13 vs. 1/2-20 vs. M12
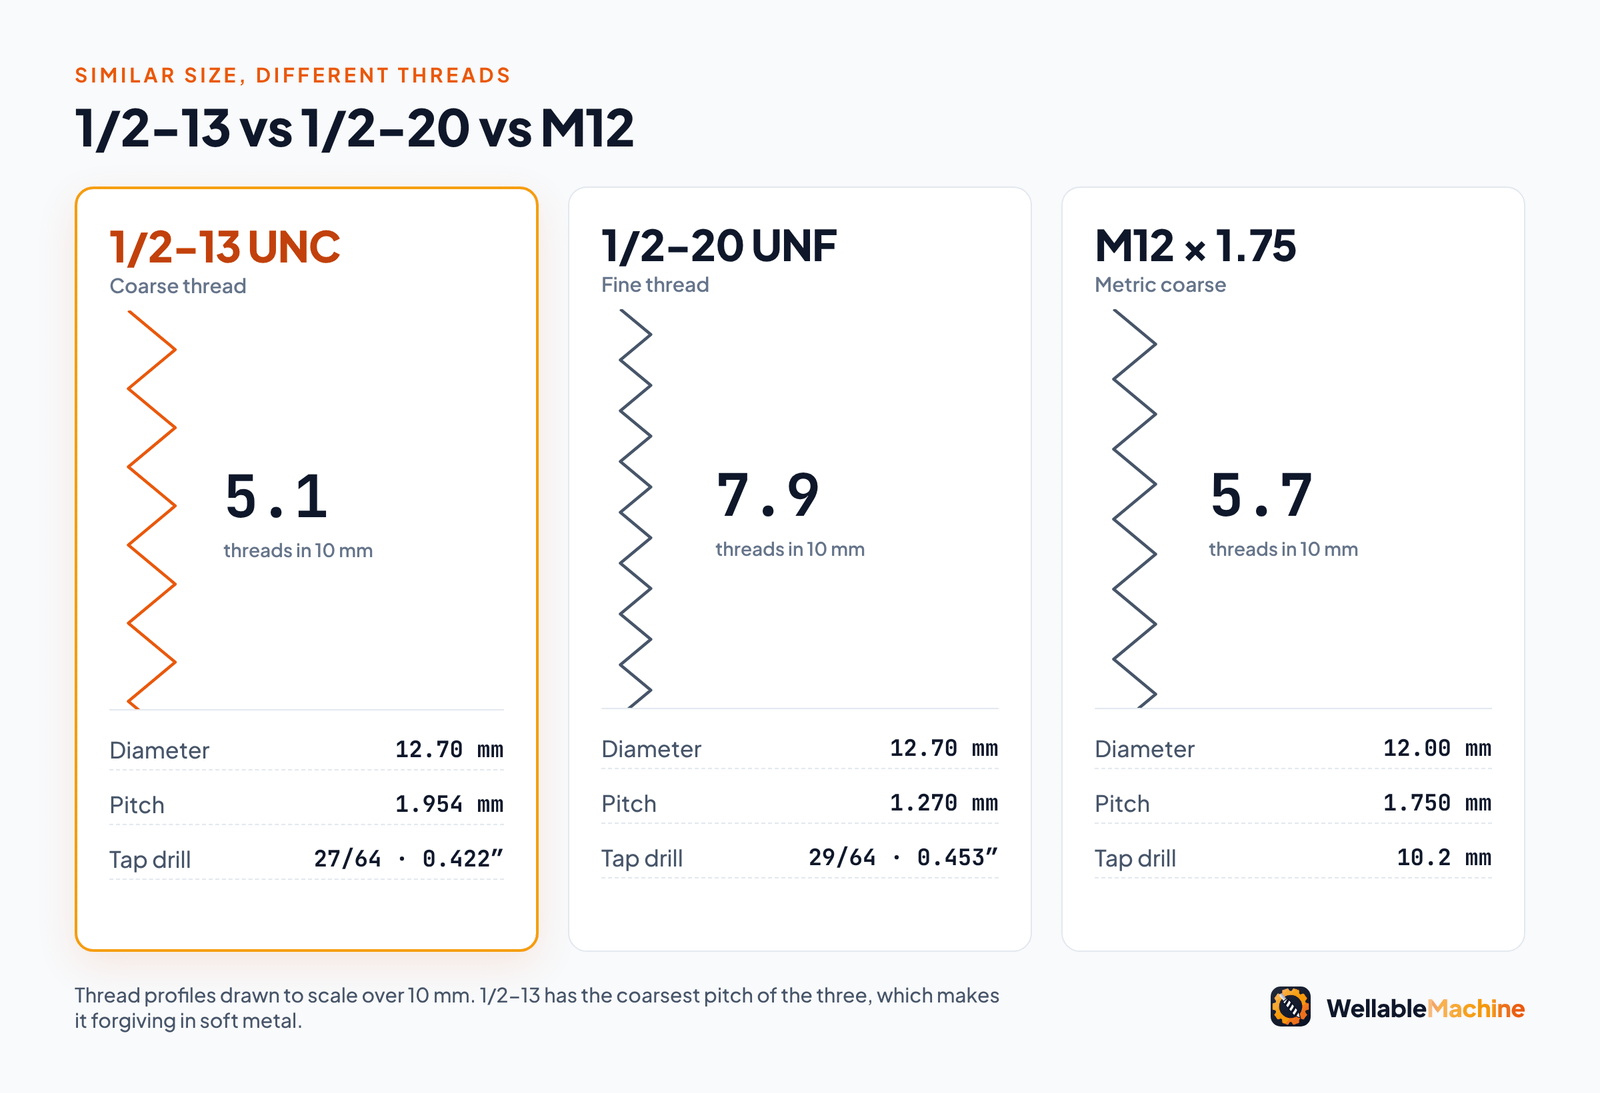
Half-inch bolts come in coarse and fine threads, and M12 is the closest metric bolt. M12 is 0.7 mm smaller in diameter, so it will be loose and strip in a 1/2-13 hole.
| Thread | Diameter | Pitch | Tap drill | Typical use |
|---|---|---|---|---|
| 1/2-13 UNC | 12.70 mm | 1.954 mm (13 TPI) | 27/64 in | Structural and general machinery |
| 1/2-20 UNF | 12.70 mm | 1.270 mm (20 TPI) | 29/64 in | Automotive, wheel studs, hydraulics |
| M12 × 1.75 | 12.00 mm | 1.75 mm | 10.2 mm | Metric machinery and vehicles |
Other 1/2 in Hole Sizes You Might Need
- Forming (roll) tap: about 0.466 in, which is 15/32 in or 11.8 mm. Forming taps this large need a lot of torque and are mainly used in machines.
- Heli-Coil / STI insert: a 17/32 in drill, then a 1/2-13 STI tap.
- Counterbore for a socket head cap screw: 13/16 in diameter, 1/2 in deep.
- Threaded rod in concrete: that’s an anchor job, not tapping. Use the anchor maker’s hole size, often 9/16 in or 5/8 in.
How to Drill and Tap a 1/2-13 Hole
- Center punch and pilot drill. Start with a 1/8–3/16 in pilot. Large drills have a wide chisel edge that won’t start accurately on their own.
- Step up if needed. On a hand drill, go pilot → 1/4 in → 27/64 in. On a drill press, pilot → 27/64 in is usually fine.
- Use the right speed. A 27/64 in drill runs about 400–500 RPM in mild steel, 200–300 RPM in stainless, and 1,000+ RPM in aluminum. Use cutting oil in steel.
- Chamfer the hole to just over 1/2 in diameter.
- Start the tap square. Use the drill press spindle or a tap guide block. A large tap that starts crooked will cut a crooked thread all the way down.
- Use a two-handle wrench and steady, balanced pressure. Half a turn forward, a quarter back, with lots of tapping fluid.
- For blind holes, drill at least 0.25 in deeper than the needed thread, and finish with a bottoming tap.
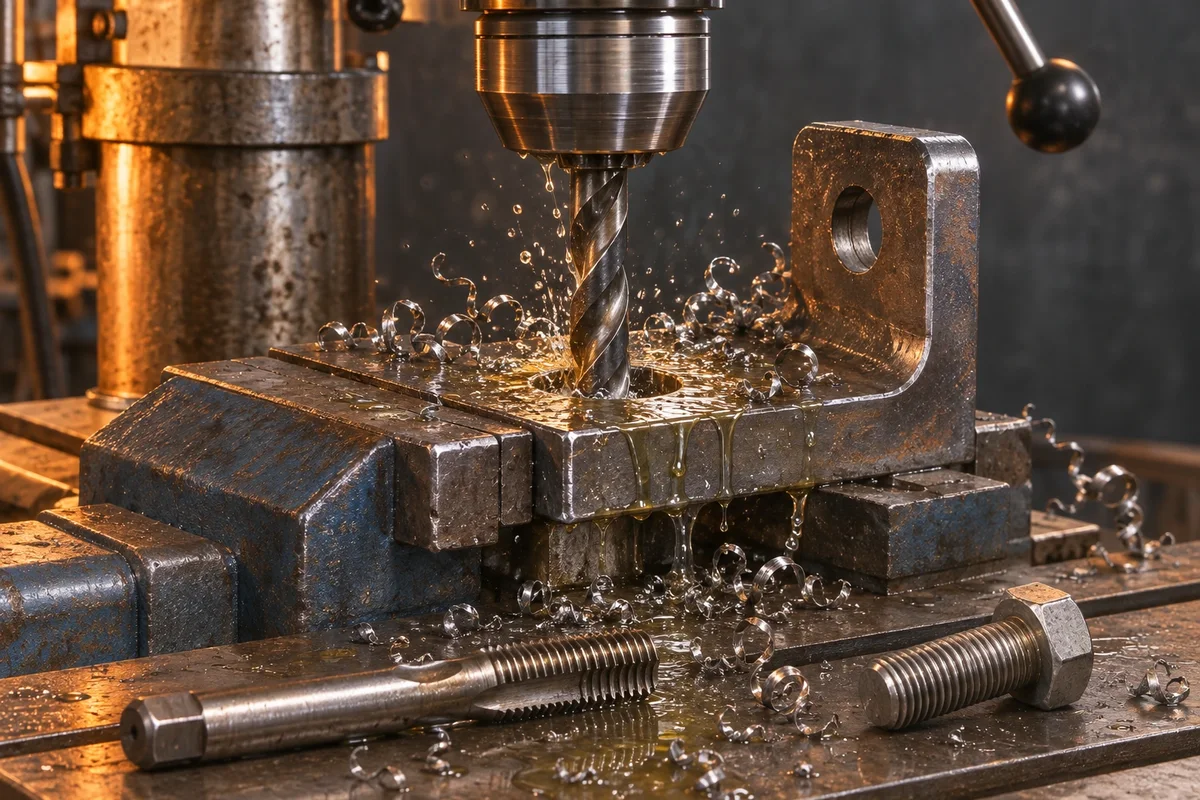
Drilling half-inch holes in stainless steel needs low speed and constant feed so the metal doesn’t harden; our how to drill stainless steel guide explains why. Cobalt bits from our list of the best drill bits for stainless steel are the right tool.
Which 1/2-13 Tap Should You Use?
| Tap type | Best for | Notes |
|---|---|---|
| Taper tap | Starting by hand | Spreads the cut over many teeth; easier on your arms |
| Plug tap | Most through-holes | The standard choice |
| Bottoming tap | Blind holes | Only after a taper or plug tap |
| Spiral point tap | Through-holes, machine tapping | Fast and strong |
| Spiral flute tap | Blind holes, machine tapping | Pulls chips out of deep holes |
For hand tapping a 1/2-13 hole in steel, a taper tap followed by a plug tap is the easiest path. The taper tap does most of the cutting, and the plug tap finishes the thread.
How Deep Should a 1/2-13 Thread Be?
- Steel: 1 × diameter, 1/2 in.
- Cast iron: 1.5 × diameter, 3/4 in.
- Aluminum: 2 × diameter, 1 in, or use a steel Heli-Coil.
Deeper threads cost a lot of effort for very little strength. If you need more holding power, use a higher-grade bolt or a through-bolt with a nut.
Common 1/2-13 Tapping Problems (and Fixes)
- Tap is too hard to turn: switch to a 7/16 in drill for hand tapping, and use more cutting fluid.
- Thread is crooked: start the tap in a drill press or with a guide block.
- Drill grabs when breaking through: reduce feed at breakthrough and clamp the work. Large drills can spin a part dangerously.
- Bolt is loose: the drill cut oversize. A dull or poorly sharpened drill cuts big holes; see how to sharpen drill bits.
- Stripped thread: repair with a 1/2-13 Heli-Coil.
Tapping 1/2-13 in Different Materials
At this size, the material you are tapping makes a big difference in how much force the tap needs.
| Material | Recommended drill | Tapping fluid | Tips |
|---|---|---|---|
| Aluminum | 27/64 | Light oil or WD-40 | Large chips; back out every turn to clear them |
| Mild steel | 27/64 (machine) or 7/16 (hand) | Sulfurized cutting oil | Taper tap first, then plug tap |
| Cast iron | 27/64 | Dry or air blast | Powder chips; blow out before assembly |
| Stainless (304/316) | 7/16 | Heavy tapping paste | Cobalt tap, two-handle wrench, slow and steady |
| Structural steel plate | 7/16 | Cutting oil | Consider a through-bolt and nut instead |
| Hardwood | 27/64 | None | Wood threads are weak; a threaded insert is better |
If you need many 1/2-13 holes in thick steel, a magnetic drill with a tapping attachment or a radial drill press will save your arms and give straighter threads.
Hand Tapping vs. Power Tapping
A 1/2-13 tap needs a lot of torque, so for more than a few holes, power tapping saves a lot of effort.
- Hand tapping is best for one-off holes, repairs and hard materials. It gives you a feel for the cut, so you can stop before the tap breaks. Use a taper or plug tap and reverse often to break chips.
- Drill press tapping (spindle turned by hand, power off) keeps the tap perfectly square. It is the easiest way to get straight threads without special tools.
- Power tapping with a tapping head, a tapping drill or a CNC machine is much faster for batches. Use spiral point taps for through-holes and spiral flute taps for blind holes, and keep the speed low: roughly 60–150 RPM in steel and up to 300 RPM in aluminum.
- Cordless drill tapping works in thin aluminum and mild steel with a combination drill-tap or a spiral point tap, set to low speed and low clutch. Avoid it in stainless and blind holes.
Frequently Asked Questions
7 quick answers from our editors
01What size drill bit for a 1/2-13 tap?
A 27/64 in drill (0.4219 in). It gives about a 78% thread.
02Can I use 7/16 for a 1/2-13 tap?
Yes. 7/16 in gives about a 63% thread, which is strong enough for most jobs and much easier to tap by hand.
03What metric drill for a 1/2-13 tap?
10.8 mm (about 75%) or 10.7 mm (about 79%).
04What size drill for 1/2-20 fine thread?
A 29/64 in drill (0.4531 in).
05What size clearance hole for a 1/2 in bolt?
33/64 in for a close fit, 17/32 in for a free fit, or 9/16 in for a loose fit.
06What size Heli-Coil drill for 1/2-13?
A 17/32 in drill, then the 1/2-13 STI tap.
07Is 1/2-13 the same as M12?
No. M12 is smaller (12 mm vs. 12.7 mm) and has a 1.75 mm pitch. Use a 10.2 mm drill for M12.
Bottom Line
For a 1/2-13 thread, drill with a 27/64 in bit (0.4219 in) for a standard 78% thread, or 10.8 mm from a metric set. When hand tapping steel or stainless, 7/16 in makes the job far easier and is still plenty strong. Always pilot drill first, start the tap square and use a two-handle wrench. For smaller sizes, see our 3/8-16 tap drill size guide or the full tap drill size chart.